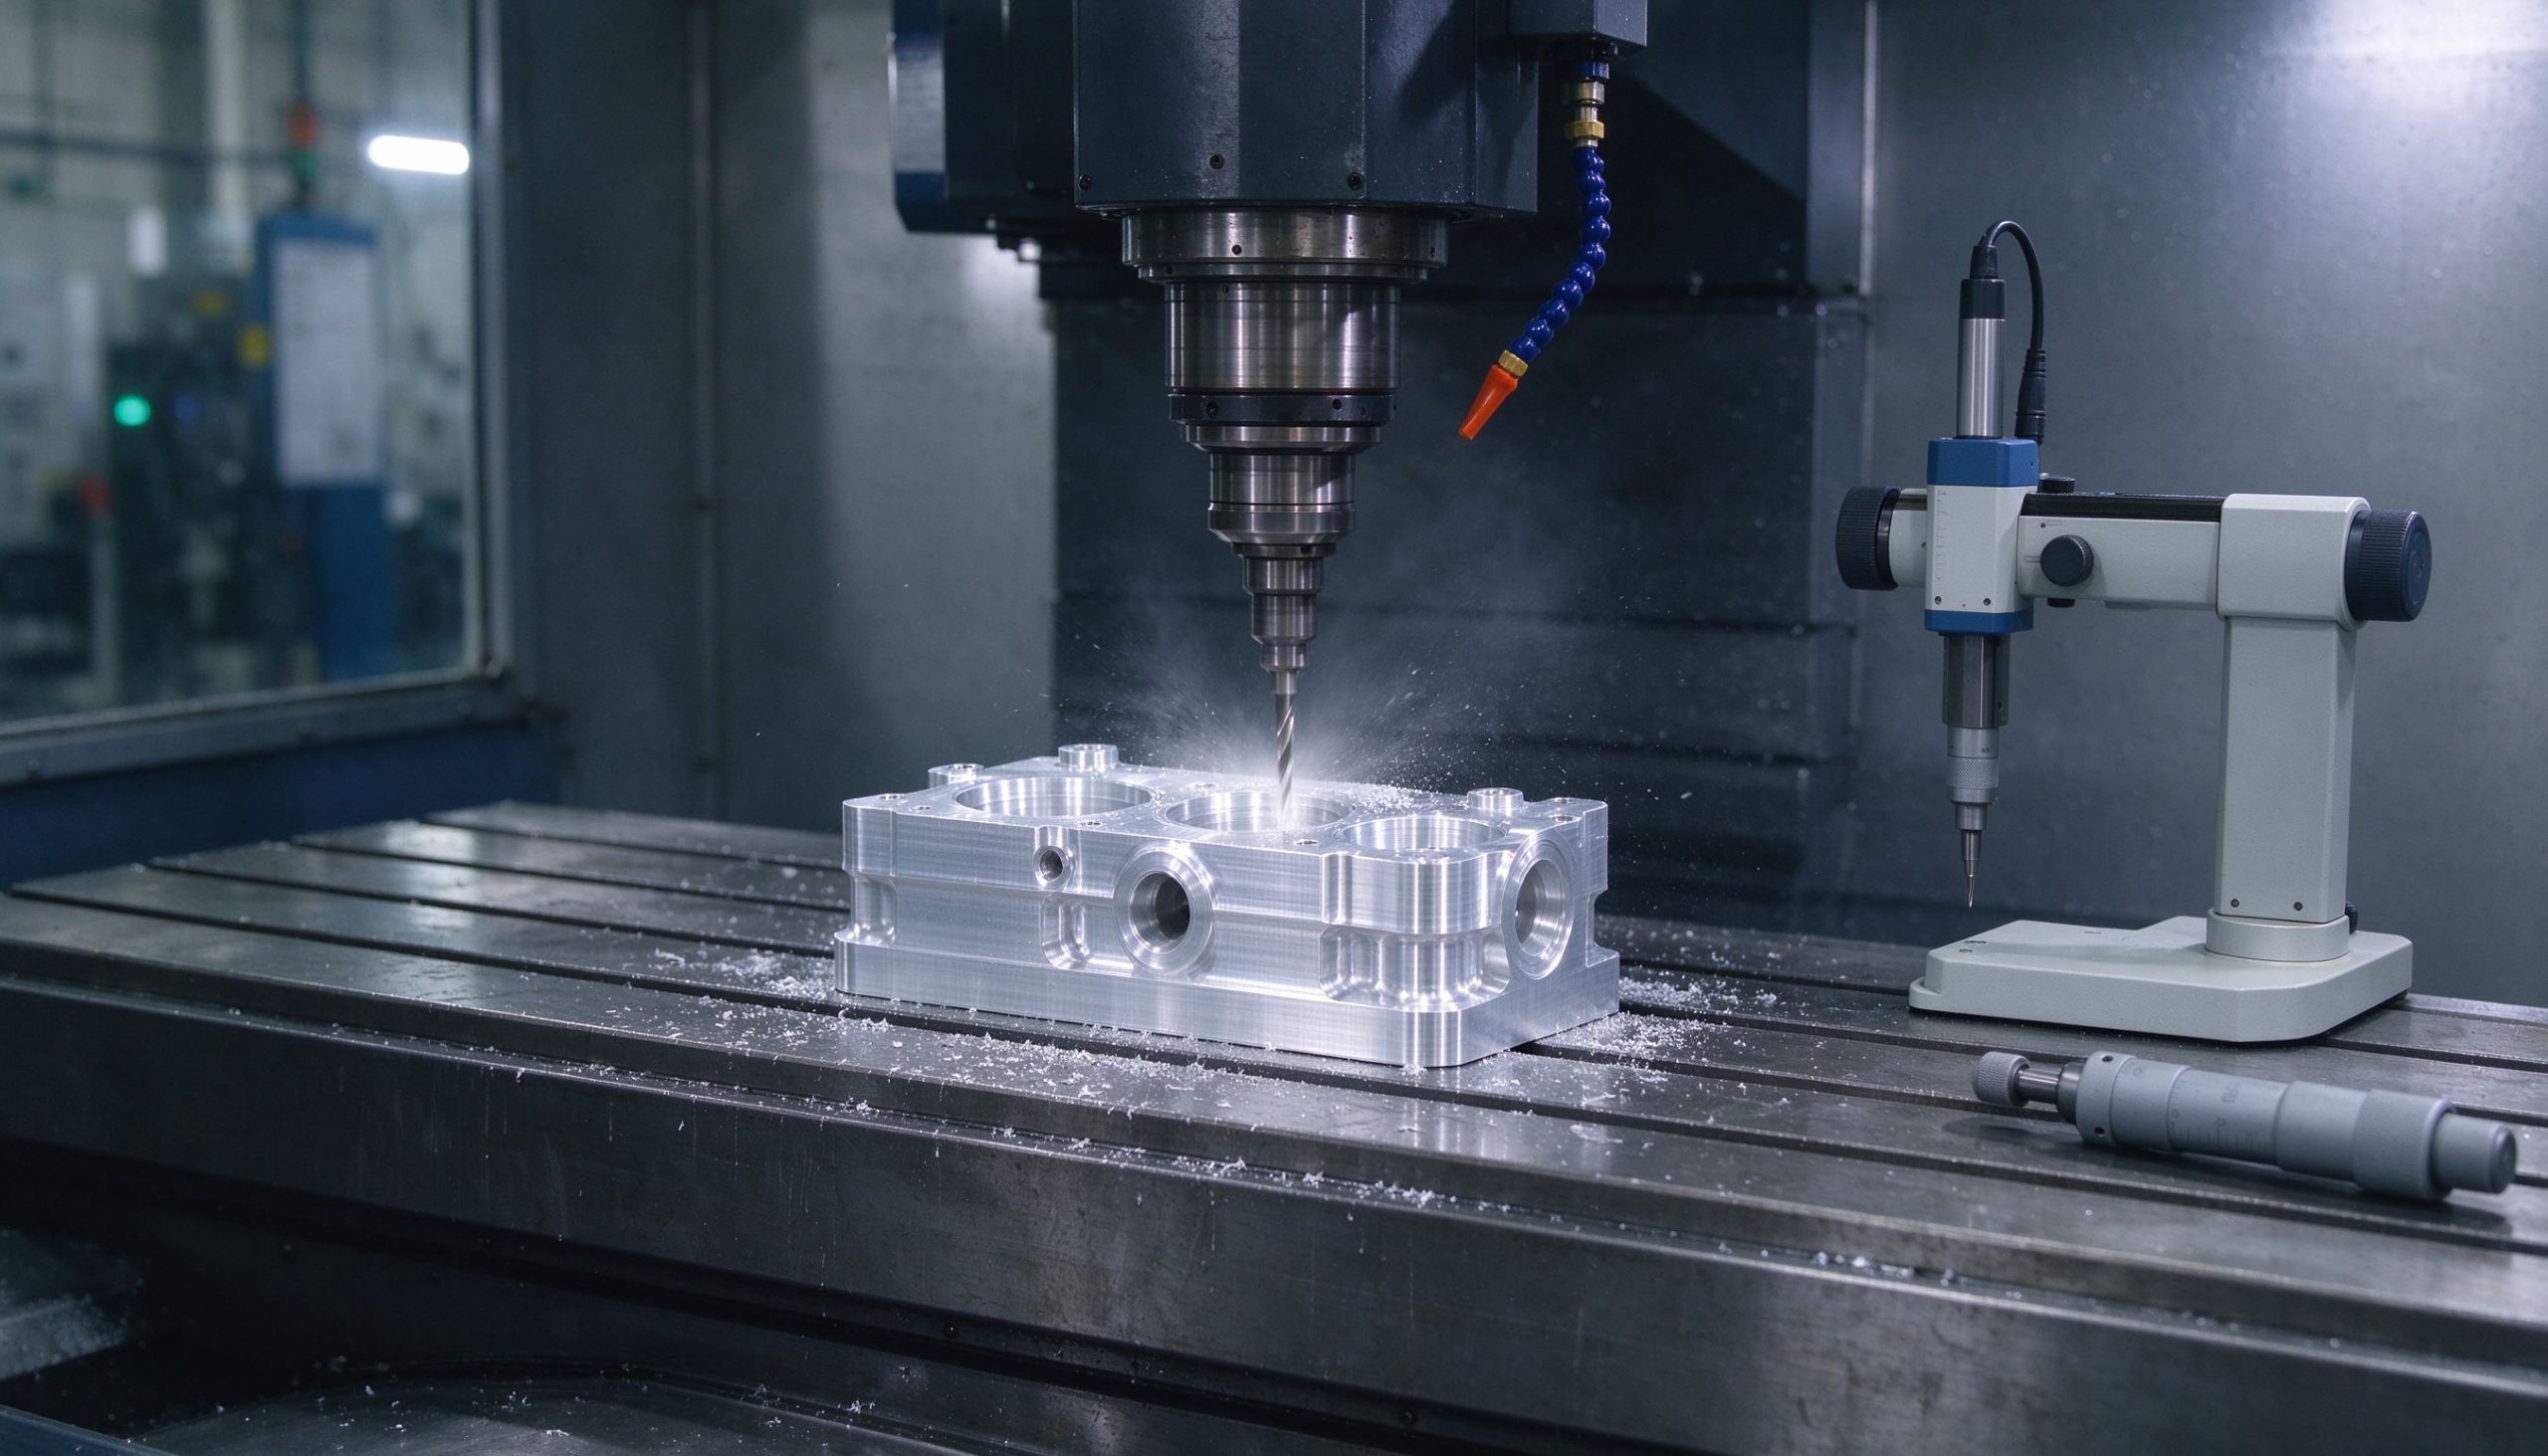
When buyers ask about 5-axis CNC machining tolerances, they usually want one number: how tight can you actually hold it? The honest answer is that a 5-axis machine does not automatically print tighter tolerances than a well-tuned 3-axis one. What it changes is how much of the part you can machine in one setup, which directly removes the largest source of tolerance error: repeat fixturing.
At PufferGo Hardware Manufacturing Factory, our 50 imported 5-axis CNC machines routinely hold ±0.005 mm on critical features. This guide explains what that number depends on, so you can specify tolerances your supplier can actually repeat across a production run rather than on a first article.
What a realistic tolerance looks like on a 5-axis mill
Most buyers confuse machine capability with part tolerance. A modern 5-axis machine may position to ±0.002 mm at the spindle, but your as-machined tolerance will always be looser because of thermal growth, tool wear, fixturing and material stress.
A practical starting point:
- ±0.01–0.02 mm on general machined features is comfortable and affordable.
- ±0.005 mm on Datum-defined critical features is achievable in controlled conditions and is the range medical and aerospace buyers specify.
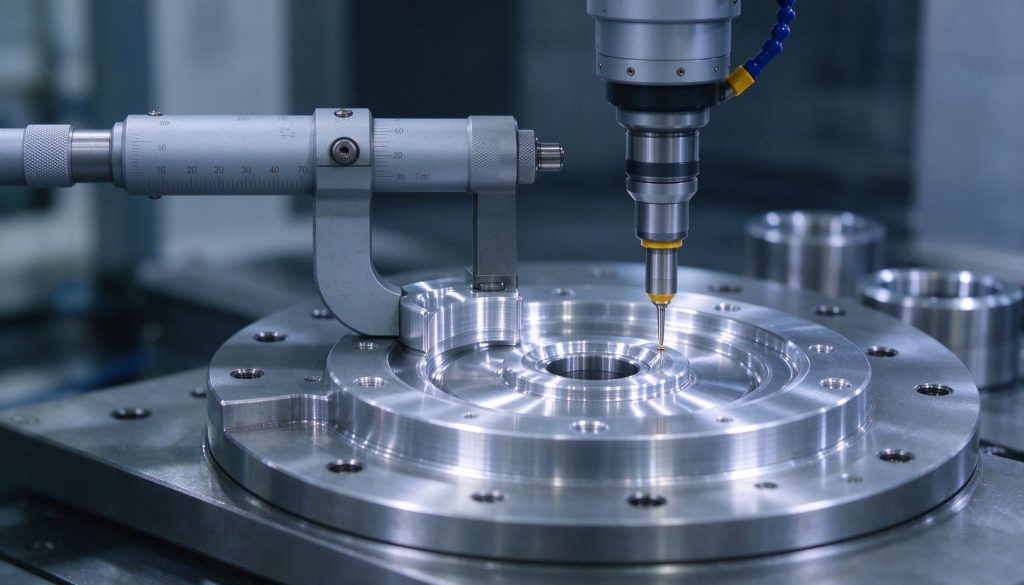
- ±0.002 mm and tighter is usually only realistic on small, stable features, with in-process measurement and a capable CMM inspection plan.
Beyond that, every extra thousandth costs disproportionately more in setup time, scrap and inspection. Over-tolerancing a drawing is one of the most common reasons a perfectly good quote comes back expensive.
Why one setup matters more than the machine spec
The core advantage of 5-axis machining is single-setup completeness. Rotating the part to access five sides means holes, datums and angled faces are all cut from one fixturing reference.
Every time a part is moved and reclamped, you introduce a small positioning error that stacks across features. A part that needs three setups may tolerate only ±0.03 mm overall even though each machine moves accurately. Machine it once on a 5-axis center and the same geometry can hit ±0.005–0.01 mm between those same features — because the reference never changes.
This is why complex impellers, housings and medical brackets move to 5-axis centers, and why our 5-axis CNC milling services is configured around datum-to-datum accuracy rather than raw spindle speed.
What actually degrades tolerance in production
Several real-world factors decide whether your ±0.005 mm survives a 1,000-piece run:
- Thermal growth. A cold spindle at 8 a.m. and a warmed one at 2 p.m. drift by micrometres. Climate control and warm-up cycles matter.
- Tool wear. End mills dull through long runs; cutting parameters and tool-change strategies must account for drift.
- Material stability. Aluminum, stainless and titanium each behave differently under clamping and release stress. We cover this in our CNC machining materials guide.
- Workholding. Thin walls and overhanging parts flex under cutting forces, no matter how accurate the axes are.
A supplier that controls these four variables, and verifies them with a CMM on a sampling plan, will hold its quoted tolerance. One that only quotes a number on paper will not.
How to specify tolerances that hold in production
- Apply tight tolerances only to the features that need them — datums, mating faces, seal surfaces. Leave the rest at general tolerance.
- Define a datum reference frame (DRF) on the drawing so the shop knows which features take priority.
- Ask for a First Article Inspection (FAI) with dimensional report before bulk production.
- Match tolerance to process. If ±0.005 mm is non-negotiable, design for a single 5-axis setup rather than a reclamped 3-axis workflow.
You can see how this plays out on our floor in the factory tour, where inspection and machining run on the same quality loop.
The bottom line
5-axis CNC machining tolerances of ±0.005 mm are realistic on well-specified, single-setup features — not as a blanket claim across every dimension on a drawing. The winning factor is not the machine nameplate; it is process control, fixturing discipline and measurement.
Founded in 2010, PufferGo runs a 12,000 m² facility in Dongguan's Chang'an precision-manufacturing cluster with 8 production lines and a 99.2% first-pass yield, exporting to 50+ countries. We hold to the standard we set ourselves: a decade of focus, only precision parts done right.
Need a tolerance review on your drawing before quoting? Contact our engineering team at sales@puffergo.com or +86 138 1234 5678 — we respond within 24 hours.
0 Comments